


Excerpt:
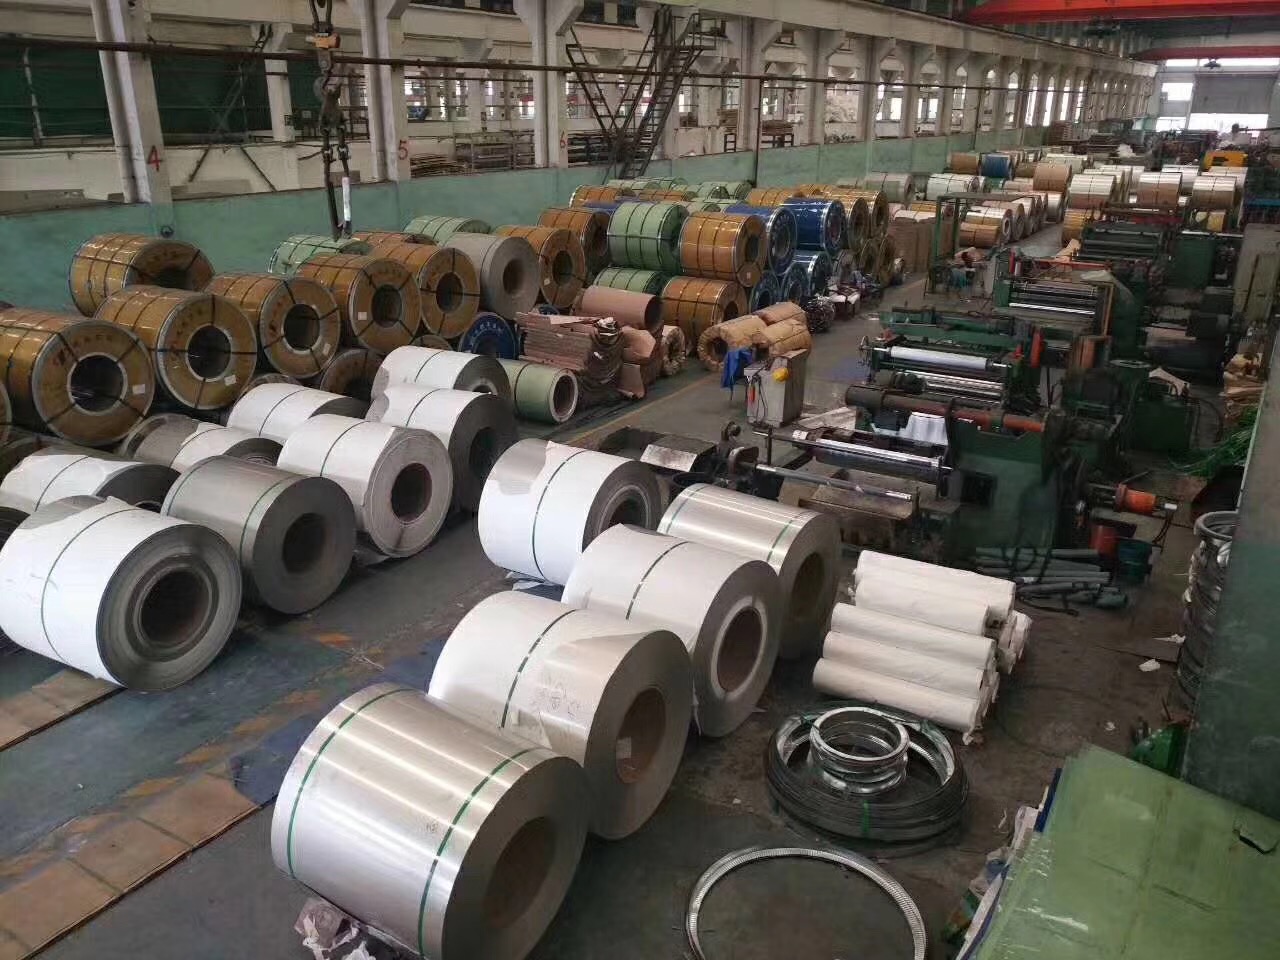
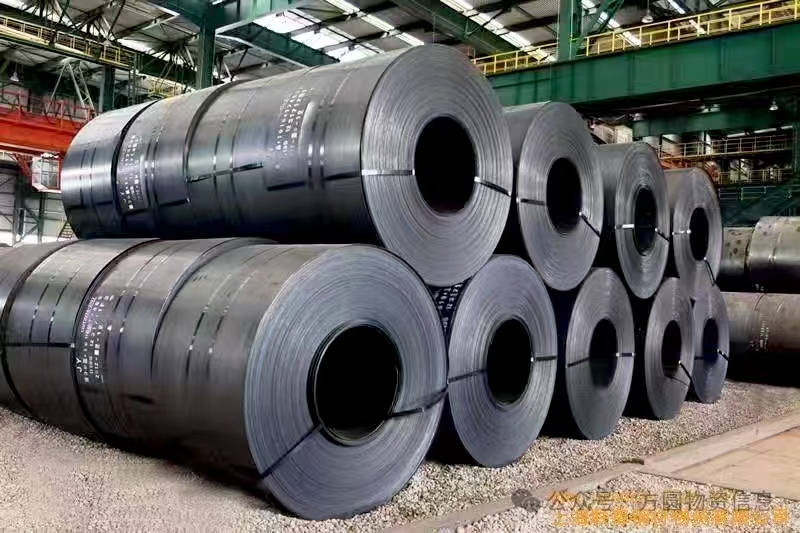
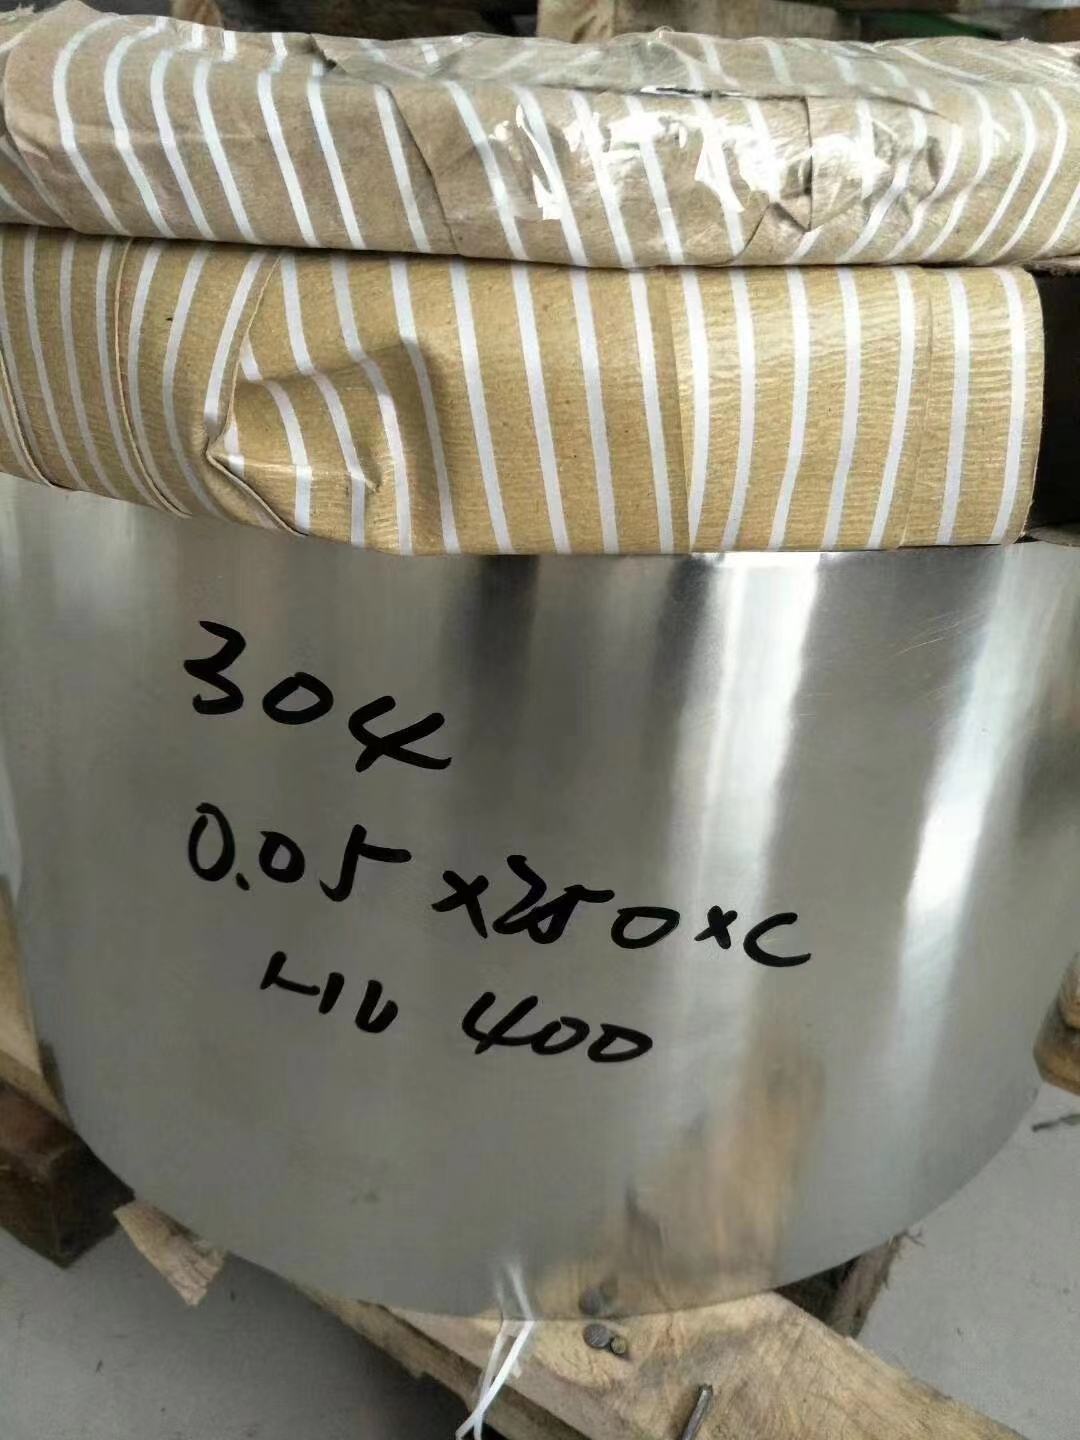
Narrow stainless strip prepared for roll forming, stamped parts, clamps and precision fabrication. The useful specification includes burr direction, width tolerance, camber and coil build as well as grade and thickness. A controlled slit-edge requirement helps the buyer plan tooling and reduce edge-related rework.
QIDA METAL · MATERIALS & EXPORT SUPPLY
304 Stainless Steel Precision Slit Strip
Narrow stainless strip prepared for roll forming, stamped parts, clamps and precision fabrication. The useful specification includes burr direction, width tolerance, camber and coil build as well as grade and thickness. A controlled slit-edge requirement helps the buyer plan tooling and reduce edge-related rework.
| Ordering item | Specification |
|---|---|
| Material / standard | ASTM A240/A240M base strip; slitting tolerances by agreement |
| Product family | Steel Coils |
| Supply basis | Enquiry-based grade, dimensions, processing and quantity; availability, MOQ and delivery confirmed in the quotation. |
| Inspection documents | Request heat/batch records and EN 10204 3.1 or other documents where required; actual document scope must be confirmed. |
01 / Selection Advantages
- Narrow-width coil enquiries can be aligned with tooling entry width and strip tracking requirements.
- Edge/burr and coil winding requirements are reviewed before slitting.
- Coil labels and pack separation help maintain heat identity when multiple widths are supplied.
02 / Specifications & Size Schedule
Use the following options to prepare a complete enquiry. The lists do not imply that every dimension combination is stocked or interchangeable with another standard. State the required tolerances and quantity for each line.
| Parameter | Enquiry requirement |
|---|---|
| Thickness / mm | 0.2, 0.3, 0.4, 0.5, 0.6, 0.8, 1.0, 1.2, 1.5, 2.0 |
| Slit width / mm | 10, 15, 20, 25, 30, 40, 50, 75, 100, 150, 200, 300, 400, 600 |
| Coil inside diameter / mm | 508 or 610 enquiry options; confirm tooling suitability |
| Condition | Annealed; cold-worked temper must be ordered separately |
| Finish | 2B / BA or agreed finish; coil weight and weld policy to be confirmed |
| Thickness band / mm | Width enquiry / mm | Define before slitting |
|---|---|---|
| 0.2–0.5 | 10–300 | Burr height, camber and winding tension |
| 0.6–1.0 | 15–400 | Width tolerance and edge condition |
| 1.2–2.0 | 20–600 | Tooling clearance and maximum coil mass |
03 / Chemical Composition
Composition is expressed in weight percent. Maximum and minimum limits refer to the listed grade/product reference; final acceptance follows the agreed standard edition and heat analysis.
| Element | Grade reference / wt.% |
|---|---|
| C | ≤0.07 |
| Mn | ≤2.00 |
| P | ≤0.045 |
| S | ≤0.030 |
| Si | ≤0.75 |
| Cr | 17.5–19.5 |
| Ni | 8.0–10.5 |
| N | ≤0.10 |
| Fe | Balance |
Composition follows ATI’s published 304 flat-product reference; the actual ordered standard edition and heat analysis govern acceptance.
04 / Mechanical Properties & Technical Notes
| Material condition | Min tensile / MPa | Min proof / MPa | Elongation reference |
|---|---|---|---|
| Annealed 304 flat-stock reference | 515 | 205 | 40%; thickness/specimen provisions apply |
The dimensional matrix is a requested processing range, with combinations confirmed against the mother coil and slitting plan. Narrow/thin strip specimens may require different elongation provisions. Do not apply annealed mechanical values to a hard-rolled temper.
05 / Processing & Inspection
| Control point | What to agree or inspect |
|---|---|
| Before slitting | Confirm grade/heat, mother-coil thickness, surface and width nesting. |
| Slit quality | Measure width, burr, edge wave, camber and telescoping to agreed limits. |
| Coil build | Agree ID/OD, winding direction, weld allowance and piece/coil mass. |
| Traceability | Transfer mother-coil identity to every slit-coil label and packing record. |
Include additional tests, third-party inspection, marking transfer and processing requirements before order confirmation. Qida can coordinate the agreed inspection scope and supporting records; an online product guide is not a delivered-batch test certificate.
06 / Export Packaging & Transport
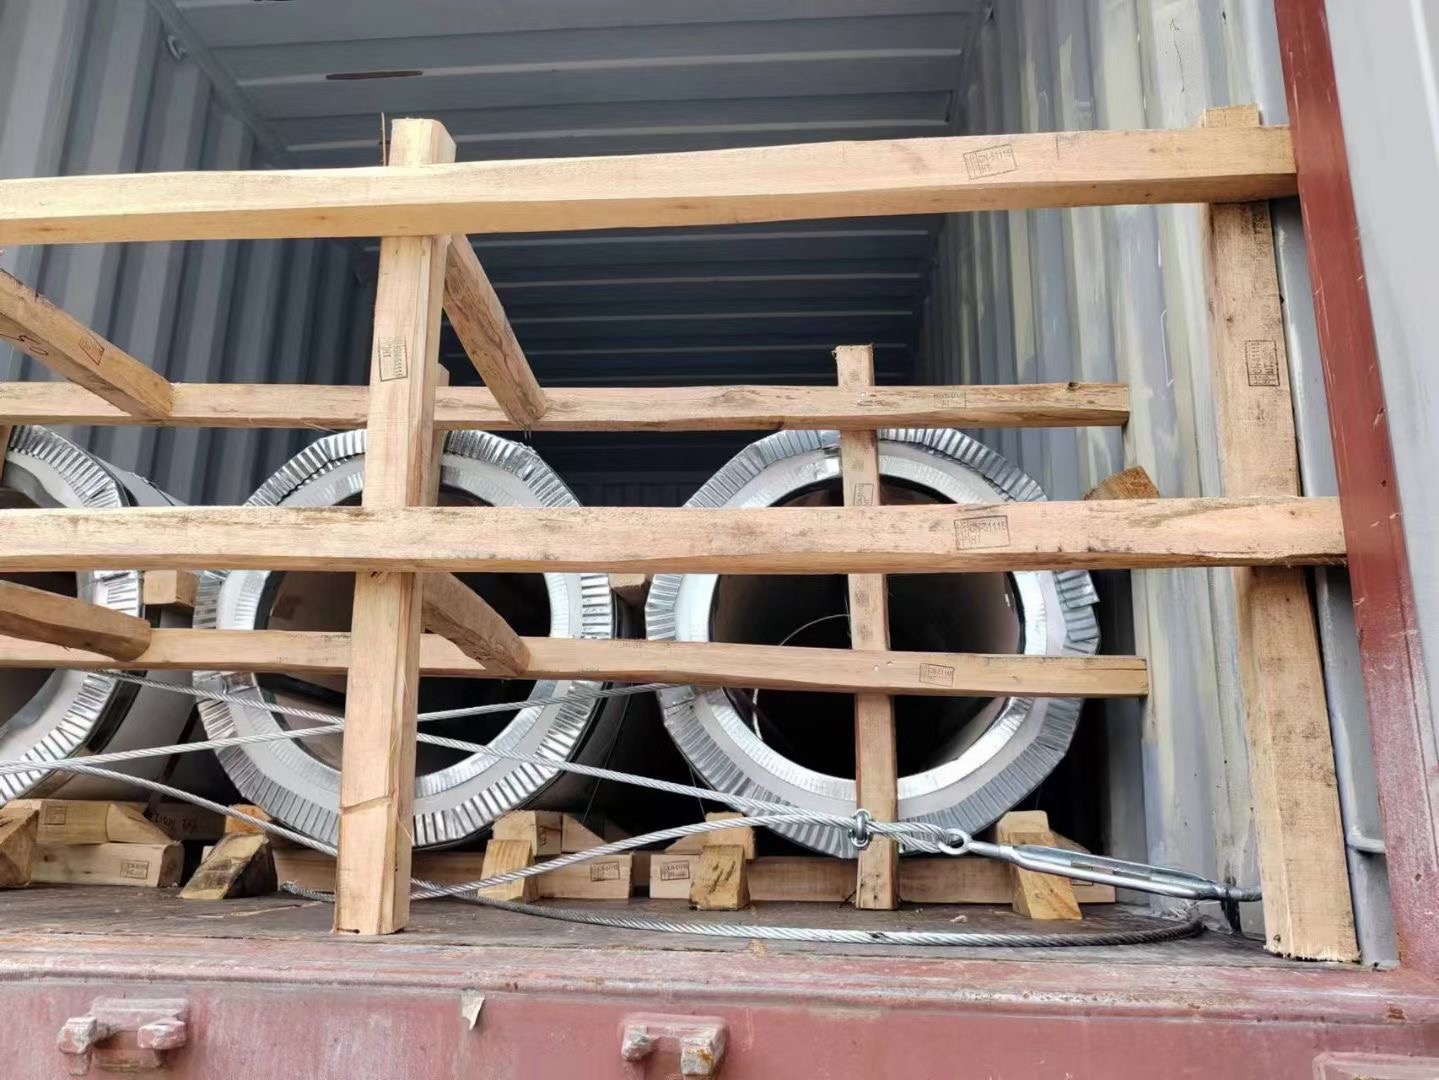
| Packing item | Practical requirement |
|---|---|
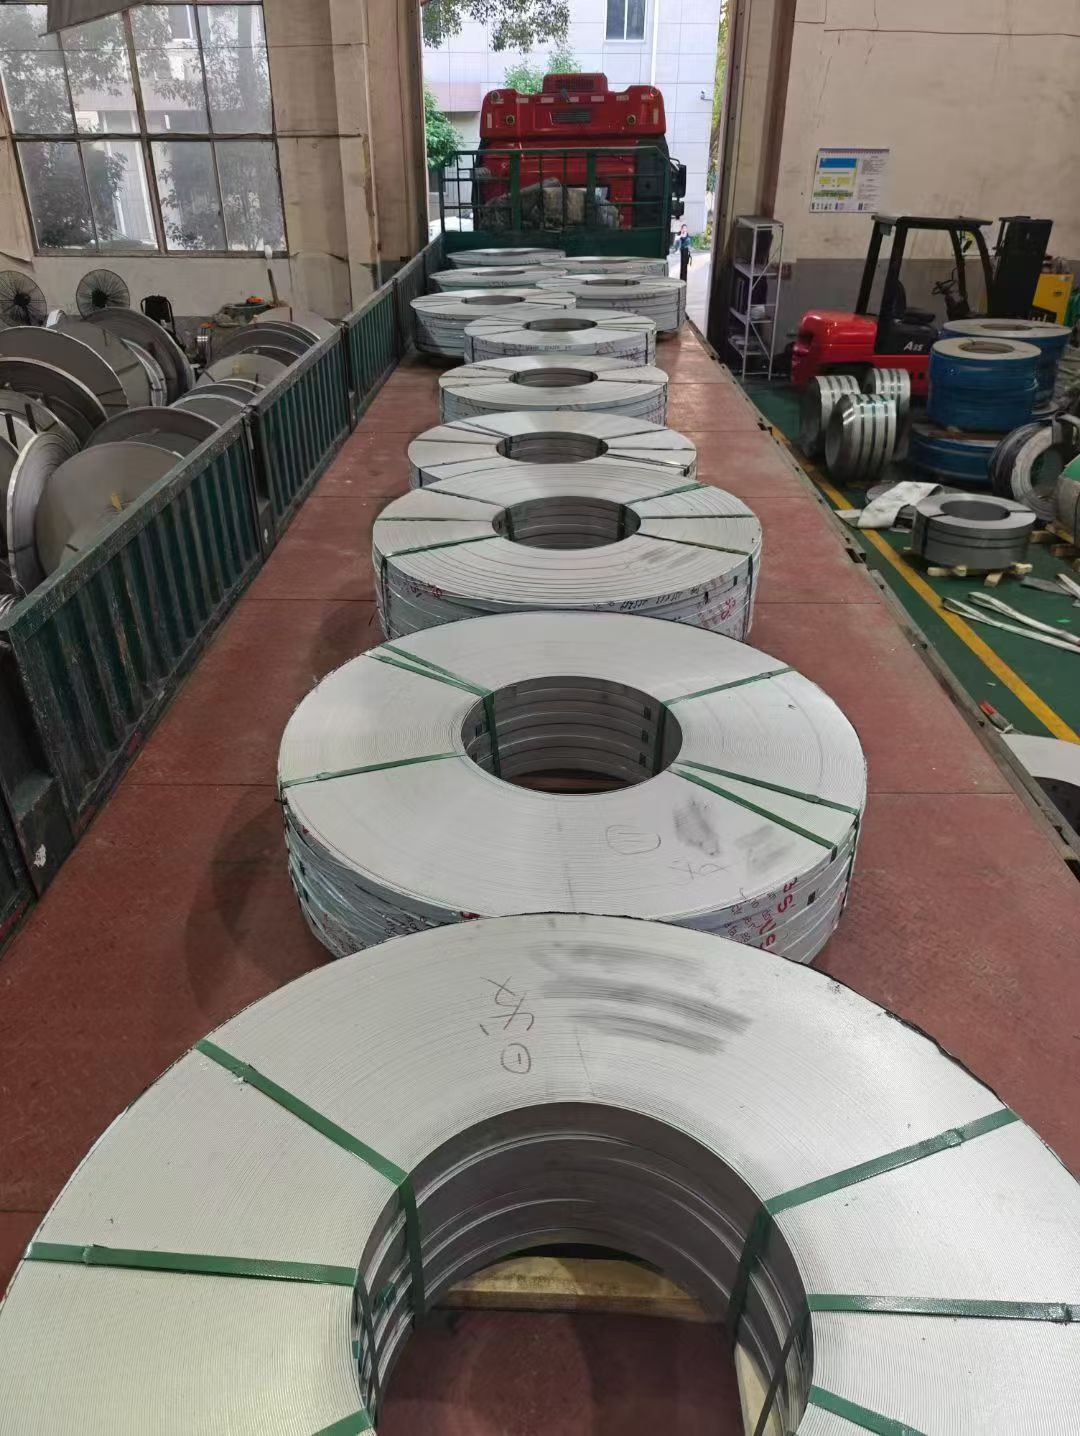
| Eye orientation | Agree eye-to-sky or eye-to-wall handling and pallet layout. |
| Edge protection | Use bore/edge guards and suitable straps to avoid edge crushing. |
| Moisture control | Protect surfaces with clean transit-appropriate wrapping and dry storage. |
| Pack marks | List grade, heat, thickness, width, net mass and coil number. |
Agree destination port, Incoterms rule and named place, package mass, unloading equipment and required shipping documents. Container capacity depends on payload limits, route and load distribution. For regulated solid-wood packaging, confirm the applicable ISPM 15 treatment and marking requirements.
07 / Qida Procurement Support
| Order stage | Our coordination | Buyer benefit |
|---|---|---|
| Specification review | Review material, dimensions, units, drawings and destination requirements. | A clear line-by-line enquiry helps reduce omissions and incompatible substitutions. |
| Processing plan | Confirm cutting, finishing, inspection and identification items in writing. | The buyer can assess scope and acceptance before production or sourcing proceeds. |
| Packing & dispatch | Coordinate labels, packing list, suitable protection and shipping-document requirements. | Piece count and heat/lot correspondence can be checked at agreed milestones. |
| After-sales follow-up | Review order references, arrival photos and inspection records for reported issues. | A documented issue description supports a specific response and follow-up. |
08 / Request a Detailed Quotation
Send the standard and edition, grade, size schedule, quantity per size, material condition, finish, processing drawings, tests/documents, packing requirements and destination port. Include maximum piece or package weight and any project approval requirements. Pricing, minimum quantity and lead time will be confirmed against the actual requirement.
Shandong Qida Metal Technology Co., Ltd. · Liaocheng, Shandong, China
qidamt@163.com · +86 139 6951 8618
Technical References
The primary references below support material selection and enquiry preparation. They do not certify a delivery batch or imply an affiliation with their publishers. Product form, condition, standard edition and supplementary requirements must be agreed in the purchase specification.